
Precast Pole Mould Guide
Column Pole Mould Shutter Straightness: Bowing, Joint Contact and Pole-Face Accuracy
Straight shutters are essential for producing precast column poles with uniform faces, consistent cross-sections and properly aligned grooves. Bowed plates, damaged stiffeners or uneven joint contact can distort the finished pole. This guide explains straightness measurement, joint inspection and maintenance of heavy-duty iron column pole moulds.
By Paras Steel Industries ·
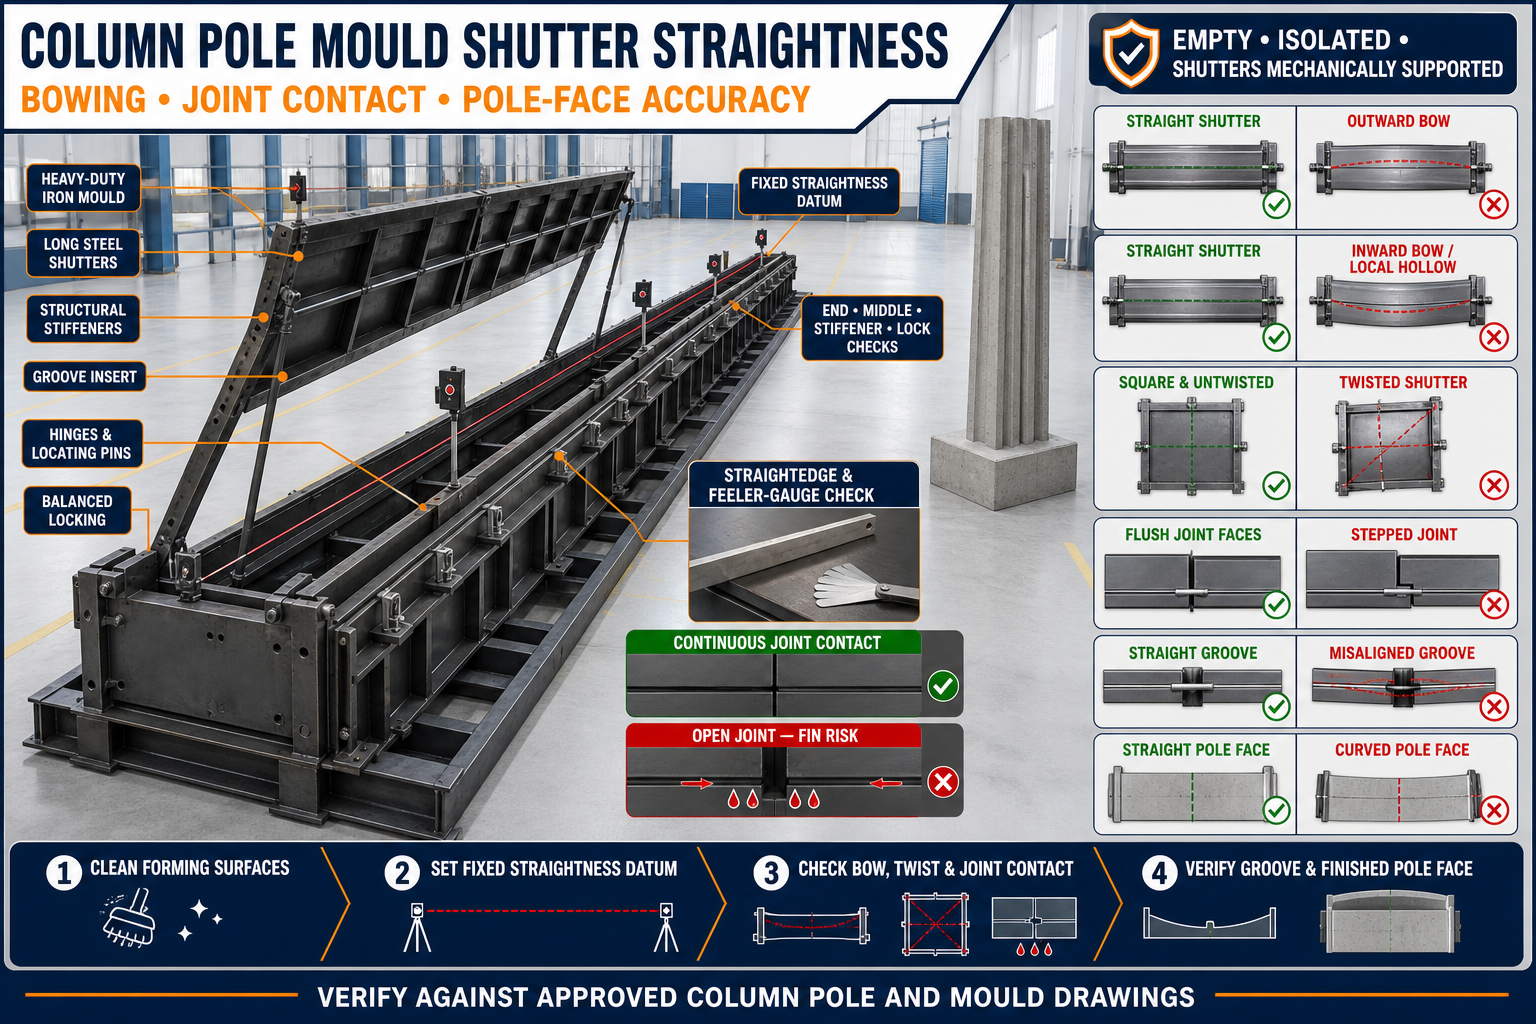
Column Pole Mould Shutter Straightness: Bowing, Joint Contact and Pole-Face Accuracy
Column Pole Mould Shutter Straightness: Bowing, Joint Contact and Pole-Face Accuracy
A precast column pole mould should produce concrete poles with straight faces, accurate dimensions and consistent profiles throughout their length.
The forming shutters control the pole’s outer surfaces. If a shutter becomes bowed, twisted or incorrectly locked, the deformation can be transferred directly to the finished concrete pole.
Regular shutter-straightness and joint-contact checks help reduce dimensional variation, concrete fins, uneven grooves and difficult panel installation.
What Is a Column Pole Mould Shutter?
A shutter is a movable or removable iron plate that forms one face of the concrete pole.
A column pole mould may contain:
• Base forming plate • Side shutters • Top or closing shutter • End shutters • Groove inserts • Chamfer strips • Structural stiffeners • Hinges • Quick locks • Locating pins • End stops • Base frame • Hydraulic or mechanical opening components
The exact arrangement depends on the required pole profile.
What Is Shutter Straightness?
Shutter straightness describes whether the forming surface follows the approved straight reference along its complete length.
A shutter may have:
• Overall bow • Local bulge • Local hollow • Edge waviness • Twist • Joint step • End displacement • Permanent deformation
A shutter can appear straight visually while still containing measurable local distortion.
What Is Shutter Bowing?
Bowing is a gradual curve along the length or width of the shutter.
The shutter may bow:
• Inward toward the concrete cavity • Outward away from the cavity • Along its complete length • Between two stiffeners • Near the middle • Near one end • Around a repaired area
Inward bowing may reduce the pole section, while outward bowing may increase it.
Why Pole-Face Accuracy Is Important
Accurate forming faces help provide:
• Straight concrete pole surfaces • Consistent pole dimensions • Uniform groove profiles • Better boundary-panel fitting • Consistent reinforcement cover • Easier stacking • Improved site installation • Reduced grinding and repair • Lower product rejection • Repeatable production quality
The finished product should always be checked against the approved drawing.
Types of Column Pole Profiles
Column pole moulds may manufacture:
• Square poles • Rectangular poles • Grooved H-posts • Multi-groove columns • Plain columns • Project-specific profiles
Different profiles require different inspection points.
Common Signs of Shutter Distortion
Possible warning signs include:
• Pole face appears curved • Pole width changes along the length • Boundary panels do not fit the grooves • Concrete fins appear at shutter joints • One shutter is difficult to close • Locks require unequal force • Joint gaps change along the mould • Reinforcement cover varies • Finished poles do not stack evenly • Repeated grinding is required • Shutter rubs during opening • Concrete binds during demoulding
Recurring defects should be traced back to the corresponding mould face.
Common Causes of Shutter Bowing
Shutter bowing may result from:
• Inadequate structural stiffening • Fresh concrete pressure • Uneven lock spacing • Damaged C-channel or H-beam stiffeners • Cracked welds • Excessive vibration • Impact during handling • Improper lifting • Uncontrolled repair welding • Thermal distortion • Concrete buildup • Foundation movement • Loose base supports • Incorrect hydraulic adjustment • Long-term wear
The cause should be identified before the shutter is repaired.
Heavy-Duty Iron Column Pole Mould Construction
A reliable mould may include:
• Smooth steel forming plates • Longitudinal stiffeners • Cross stiffeners • Rigid base frame • Accurate groove inserts • Strong corner joints • Adjustable or fixed locks • Locating pins • Hinge supports • Replaceable wearing components • Suitable shutter-opening system
The structural design should match the pole dimensions and production conditions.
Preparing the Mould for Straightness Inspection
Before measurement:
• Remove the finished pole • Empty the mould • Clean all forming surfaces • Remove hardened slurry • Isolate hydraulic equipment • Release stored pressure • Mechanically support shutters • Close the mould in the specified inspection condition • Review the approved mould drawing • Identify fixed datums • Prepare suitable inspection tools
Never inspect a shutter that can move unexpectedly.
Mould Condition During Inspection
Shutter readings may change depending on whether:
• Shutters are open or closed • Locks are engaged • Hydraulic cylinders are pressurised • End shutters are installed • Groove inserts are fitted • The mould is empty or loaded • The mould is hot or cold
Use a consistent inspection condition and record it.
Establishing a Fixed Reference Datum
Suitable references may include:
• Mould-base centreline • Fixed base-frame edge • Machined forming edge • Verified end stop • Survey reference line • Approved straightness fixture
Do not measure only from another movable shutter that has not been checked.
Tools for Checking Shutter Straightness
Possible tools include:
• Long verified straightedge • Feeler gauges • Tensioned reference wire • Laser line • Survey equipment • Dial indicator • Approved profile template • Measuring tape • Engineer’s square
The selected tool should suit the mould length and required accuracy.
Checking With a Straightedge
A straightedge can identify local gaps and high points.
A general method includes:
1. Clean the Forming Surface
Remove all concrete and debris.
2. Position the Verified Straightedge
Place it along the shutter’s approved inspection line.
3. Check Both Ends
Confirm the reference contact.
4. Inspect the Middle
Look for a gap or raised area.
5. Use Suitable Gauges
Measure local clearance where required.
6. Repeat at Multiple Heights
Check upper, middle and lower regions.
7. Record Every Deviation
Mark the shutter location.
8. Compare With the Approved Requirement
Do not assume a generic tolerance.
Checking With a Tensioned Reference Wire
A tensioned wire can provide a long straight reference.
The wire should be:
• Fixed to stable reference points • Kept clear of the forming surface • Protected from disturbance • Positioned consistently • Checked for sag as required by the method
Measure the relationship between the wire and shutter at defined stations.
Checking With a Laser
A laser line can help reveal:
• Longitudinal bowing • Shutter-edge displacement • Joint steps • End misalignment • Local plate movement • Twist
The laser should be positioned independently of the mould on a stable surface.
Creating Measurement Stations
Check the shutter at:
• Both ends • Middle • Intermediate stiffener locations • Locking points • Hinge locations • Groove-insert positions • Repaired areas • Locations corresponding to product defects
Use the same stations for future inspections.
Checking Longitudinal Bow
Longitudinal bow runs along the pole length.
Check:
• Upper forming edge • Lower forming edge • Centre of the plate • Groove reference line • Structural frame • Shutter-contact edge
A plate can bow even when its outer frame appears straight.
Checking Transverse Bow
Transverse bow occurs across the width of the shutter.
It may cause:
• Rounded pole face • Changed groove depth • Incorrect pole width • Local concrete-cover variation • Poor joint contact
Check across the shutter at several stations.
Checking Local Plate Bulging
Local bulging often occurs between stiffeners.
Inspect for:
• Outward plate movement • Inward dents • Broken welds • Loose stiffeners • Corrosion behind plates • Impact marks • Previous repair heat zones
A local defect can be repeated on every pole.
What Is Shutter Twist?
Twist occurs when one corner of the shutter is displaced relative to the others.
A twisted shutter can produce:
• Rotated pole cross-section • Unequal diagonal dimensions • Joint steps • Different groove positions • Difficult locking • Uneven concrete fins
Twist should be checked separately from bowing.
Checking Shutter Twist
Possible methods include:
• Comparing corner elevations • Measuring diagonals • Laser-plane inspection • Checking joint contact at all corners • Surveying forming edges • Using an approved fixture
Do not force a twisted shutter closed using excessive lock pressure.
Checking Shutter-Joint Contact
Joint contact is the relationship between adjoining shutter edges when the mould is closed.
A correct joint should have:
• Clean contact surfaces • Continuous closure • Aligned forming faces • No significant step • Uniform seal compression where fitted • Fully engaged locating pins • Balanced locks
A joint that touches only near the locks may still leak between them.
Common Causes of Poor Joint Contact
Joint gaps may result from:
• Hardened concrete • Bowed shutter edges • Worn hinges • Loose locks • Damaged seals • Bent locating pins • Weld distortion • Groove-insert interference • Reinforcement trapped in the joint • Mould-base twist
The root cause should be corrected before adding sealing material.
Checking Joint Gaps
Inspect the complete shutter joint:
• At both ends • At every lock • Between locks • At groove inserts • Near hinges • Around chamfer strips • At the base • At end-shutter intersections
Use an approved light, gauge or contact-check method.
Checking Joint Steps
A joint step occurs when adjoining forming faces are not flush.
This may create:
• Raised concrete line • Groove misalignment • Uneven pole face • Edge damage • Additional grinding • Difficult demoulding
Check with a straightedge across the joint.
Inspecting Locating Pins and Bushes
Locating components establish repeatable shutter position.
Check:
• Pin straightness • Bush wear • Enlarged holes • Incomplete engagement • Concrete buildup • Loose mounting • Cracked welds • Unequal contact • Corrosion • Impact damage
Worn pins may allow the shutter to shift during vibration.
Inspecting Hinges
A worn hinge can allow shutter sag or sideways movement.
Inspect:
• Hinge pins • Bushes • Hinge leaves • Mounting bolts • Welds • Lubrication • Vertical movement • Binding • Opening path • Alignment
Hinge repair should restore the original shutter position.
Inspecting Locks and Clamps
Inspect:
• Wedge surfaces • Screw threads • Clamp pivots • Lock pins • Mounting brackets • Welds • Engagement • Wear • Alignment • Concrete buildup
A lock should secure the shutter without bending it.
Balanced Locking Sequence
A general procedure may include:
1. Clean Contact Faces
Remove all concrete and slurry.
2. Close the Shutter Gently
Allow locating components to engage.
3. Apply End Locks Lightly
Hold the shutter without distortion.
4. Engage Intermediate Locks
Start every lock.
5. Check Joint Contact
Inspect the complete length.
6. Tighten Progressively
Work in a balanced sequence.
7. Recheck Straightness
Confirm locking has not pulled the shutter.
8. Inspect Joint Steps and Gaps
Complete the pre-pour check.
Do not fully tighten one lock while nearby joints remain open.
Inspecting Structural Stiffeners
Stiffeners help resist plate bowing.
Check for:
• Bent C-channels • Twisted angles • Damaged H-beams • Cracked welds • Loose connections • Plate separation • Corrosion • Previous repair distortion • Inadequate bearing contact • Movement marks
A plate cannot remain straight if its supporting frame is damaged.
Inspecting Welds
Check welds between:
• Forming plate and stiffener • Lock bracket and frame • Hinge and shutter • Groove support and plate • Base frame and supports • End-stop components
Cracked or separated welds can allow local plate movement.
Groove-Insert Alignment
Column poles used for boundary walls may contain grooves for receiving concrete panels.
Check:
• Groove straightness • Groove width • Groove depth • Centreline • Taper • Insert attachment • End transitions • Relationship with the opposite groove
A straight shutter with a misaligned insert can still produce an inaccurate pole face.
Chamfer-Strip Alignment
Chamfer strips should remain:
• Straight • Secure • Continuous • Aligned at corners • Free from concrete buildup • Compatible with shutter closure • Smooth for demoulding
A damaged chamfer may cause concrete fins or edge breakage.
End-Shutter Relationship
End shutters should meet the long shutters correctly.
Check:
• Pole length • End-face squareness • Joint closure • Groove termination • Chamfer transitions • Locating pins • Lock engagement • Slurry sealing
A tilted end shutter can pull long shutters out of position.
Base-Frame Alignment
The base frame provides the mould reference.
Inspect:
• Longitudinal level • Cross-level • Straightness • Support contact • Anchor condition • Foundation settlement • Welds • Structural members • Concrete buildup below supports
Do not adjust shutters before confirming the base frame.
Reinforcement Clearance
The reinforcement cage should not push the shutters outward.
Check:
• Cage dimensions • Pole centreline • Required concrete cover • Spacers • Groove clearance • End clearance • Lifting details where approved • Tie-wire position • Stability during closure
Do not force the mould closed around an oversized cage.
Applying Mould Release Agent
After cleaning and inspection, apply a suitable release agent.
The coating should be:
• Thin • Uniform • Present on all forming faces • Applied around grooves • Applied along chamfers • Free from excessive pooling • Kept away from reinforcement
Release agent cannot correct a rough or bowed shutter.
Pre-Pour Straightness Checklist
Before concrete placement, confirm:
• Mould is clean • Base frame is level and straight • Shutters are installed correctly • Longitudinal straightness is checked • Transverse bowing is checked • Local bulges are inspected • Shutter twist is checked • Joint contact is continuous • Joint steps are controlled • Locating pins are fully engaged • Hinges are stable • Locks are progressively tightened • Groove inserts are aligned • Chamfer strips are secure • End shutters are square • Reinforcement has adequate clearance • No tools remain inside the mould
Record critical measurements according to the quality plan.
Concrete Placement and Shutter Movement
Uneven placement can apply unbalanced pressure.
Good practices include:
• Fill the mould progressively • Avoid overfilling one section • Prevent direct impact on shutters • Keep reinforcement centred • Monitor long shutter joints • Observe locks and supports • Follow the approved casting sequence
The selected concrete and placement procedure should match the mould design.
Effect of Vibration
Vibration can reveal loose components.
Before vibration:
• Check all locks • Confirm hinge condition • Inspect stiffeners • Verify base supports • Remove loose tools
During vibration, watch for:
• Shutter movement • Joint leakage • Lock movement • Local plate vibration • Unusual metallic noise • Changing joint gaps • Groove-insert movement
Stop the process safely if significant movement occurs.
Preparing for Demoulding
Before opening the mould:
• Confirm adequate concrete strength • Support the pole • Isolate powered equipment • Release hydraulic pressure • Mechanically support shutters • Clean concrete around locks • Identify the approved opening sequence • Keep personnel clear of pinch points • Prepare suitable handling equipment
Do not allow a long shutter to drop or twist during opening.
Correct Demoulding Sequence
A general procedure may include:
1. Support the Concrete Pole
Prevent rolling or sudden movement.
2. Clean Exposed Joints
Remove concrete around locks.
3. Release Secondary Locks
Open them progressively.
4. Support the Long Shutter
Prevent sagging after release.
5. Release Primary Locks
Follow the approved sequence.
6. Open the Shutter Evenly
Avoid dragging it across the pole face.
7. Remove End Shutters
Protect pole ends and grooves.
8. Move the Pole Safely
Use the approved handling arrangement.
9. Inspect the Finished Faces
Check straightness, fins, grooves and edges.
Never force a shutter that remains mechanically locked.
Post-Demoulding Pole Inspection
Check the finished pole for:
• Face straightness • Cross-section dimensions • Width at multiple stations • Diagonal dimensions • Groove position • Groove straightness • Pole length • End-face squareness • Concrete fins • Honeycombing • Edge damage • Surface finish • Reinforcement cover
Record each defect against the corresponding mould face.
Checking Pole-Face Straightness
A finished pole may be checked using:
• Verified straightedge • Tensioned wire • Laser line • Surveying equipment • Approved inspection fixture
Support the pole correctly during inspection to avoid misleading readings.
Troubleshooting Common Problems
Problem: Pole Face Bows Outward
Possible causes:
• Shutter plate bowed outward • Stiffener damaged • Concrete pressure opened the mould • Locks were loose • Welds cracked
Problem: Pole Face Bows Inward
Possible causes:
• Shutter plate is permanently distorted • Locking pressure is excessive • Previous repair pulled the plate inward • Support frame is twisted
Problem: Pole Width Changes Through the Middle
Possible causes:
• Long shutter is bowed • Base frame is distorted • Reinforcement pushed the shutter • Locks are uneven • Stiffener spacing or condition is inadequate
Problem: Concrete Fin Runs Along the Joint
Possible causes:
• Joint gap • Dirty contact face • Bent shutter edge • Damaged seal • Worn locating pins • Uneven lock pressure
Problem: Visible Step Appears on the Pole Face
Possible causes:
• Forming faces are not flush • Shutter is sagging • Hinge is worn • Locating pin is damaged • Lock pulls one plate out of alignment
Problem: Boundary Panel Does Not Fit the Groove
Possible causes:
• Groove insert is bowed • Groove width or depth is incorrect • Insert centreline shifted • Shutter distorted around the groove • Concrete fin remains • Panel and pole types are mismatched
Problem: Shutter Is Difficult to Close
Possible causes:
• Concrete buildup • Hinge misalignment • Shutter distortion • Reinforcement interference • Locating pins not aligned • Base frame has moved
Correcting Shutter Distortion
A controlled repair process may include:
• Measuring the full shutter • Identifying the distortion type • Inspecting supporting stiffeners • Checking foundation and base frame • Planning approved mechanical correction • Controlling welding heat • Replacing damaged structural members • Rechecking forming-surface straightness • Trial-closing the mould • Verifying joint contact
Uncontrolled heating or hammering may worsen the distortion.
Mould Maintenance Checklist
After every casting cycle:
• Clean all forming surfaces • Remove slurry from joints • Inspect shutter straightness • Check local plate condition • Inspect stiffeners • Examine welds • Check hinges and bushes • Inspect locating pins • Check locks and clamps • Clean groove inserts • Inspect chamfer strips • Verify end-shutter alignment • Lubricate approved moving points • Apply corrosion protection during storage • Record recurring product defects
Maintenance records help detect gradual shutter deformation.
Benefits of Accurate Shutter Straightness
Straight, correctly aligned shutters provide:
• Straighter pole faces • Consistent cross-sections • Better groove alignment • Reduced concrete fins • Improved panel fitting • Controlled reinforcement cover • Easier demoulding • Lower finishing work • Reduced rejection • Longer mould service life
Conclusion
Column pole mould shutter straightness directly affects the pole’s face accuracy, cross-section and groove alignment. Long forming plates should be inspected for overall bowing, local bulges, twist and joint steps.
Reliable checks require clean forming surfaces, fixed datums and measurements at both ends, the middle, stiffener locations and locking points. Hinges, locating pins, structural stiffeners, groove inserts and the base frame should also be inspected.
A properly maintained heavy-duty iron column pole mould helps manufacturers produce straight precast poles with consistent faces, accurate grooves and dependable boundary-wall installation.