
Precast Mould Guide
U Drain Mould Inner-Core Centring: Equal Wall Thickness, Taper and Clearance Checks
The inner core forms the internal channel of a precast U Drain. If it is off-centre, tilted or incorrectly locked, the two walls may have different thicknesses and the drain can become difficult to install or demould. This guide explains core centring, taper, clearance and pre-pour checks for heavy-duty iron U Drain moulds.
By Paras Steel Industries ·
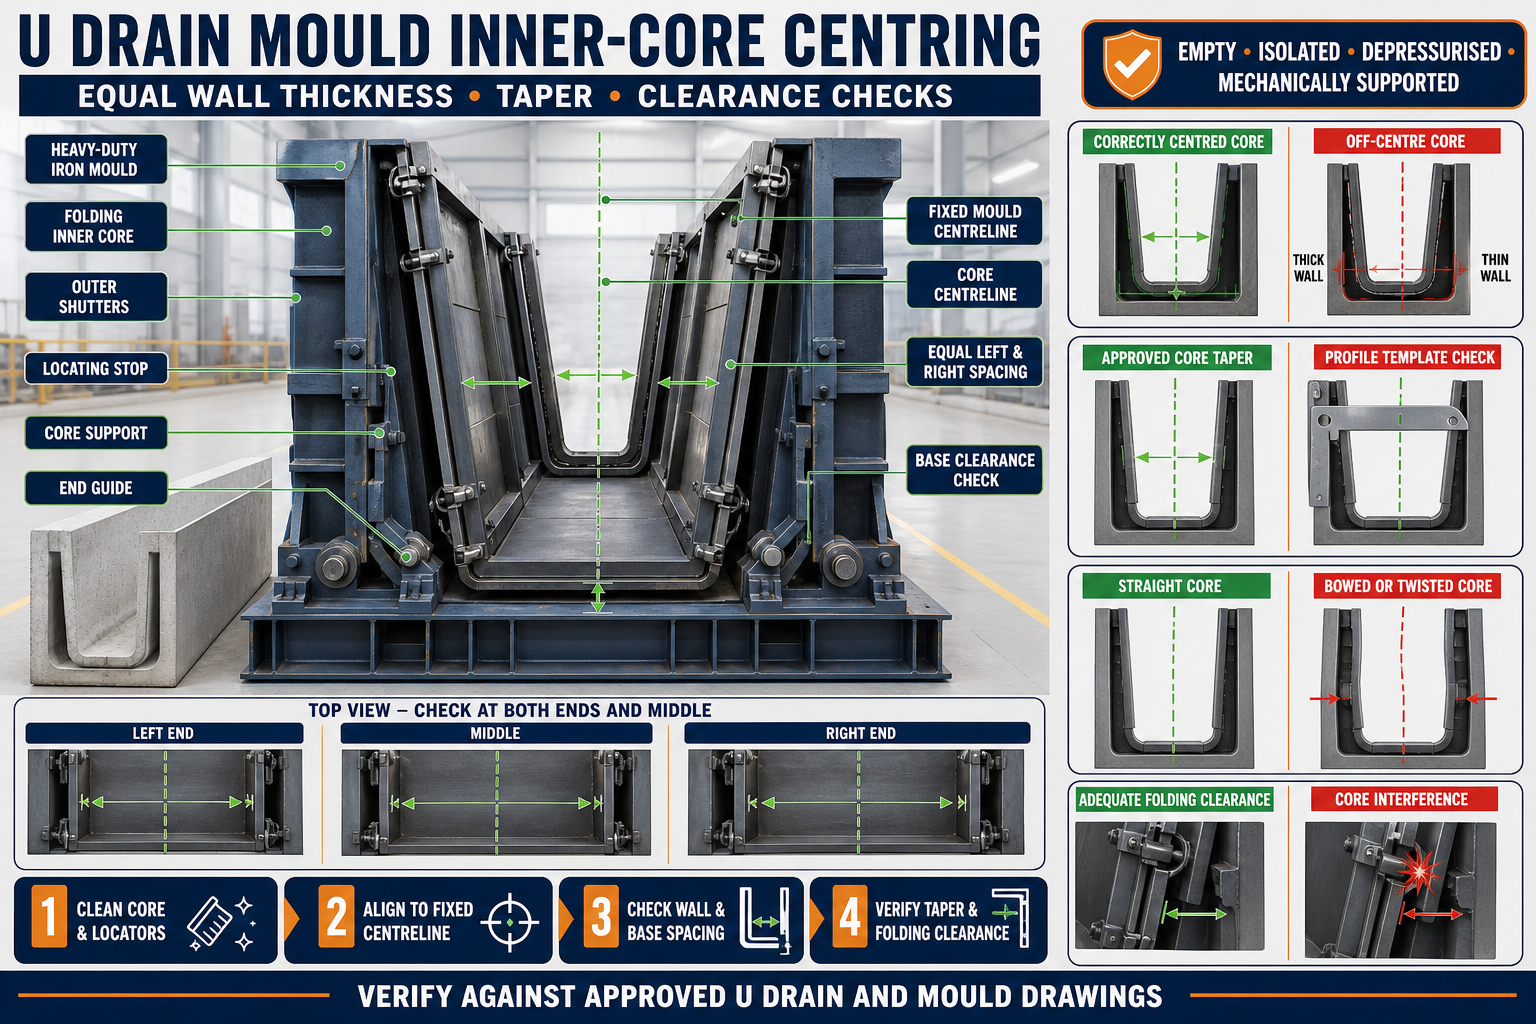
U Drain Mould Inner-Core Centring: Equal Wall Thickness, Taper and Clearance Checks
U Drain Mould Inner-Core Centring: Equal Wall Thickness, Taper and Clearance Checks
A precast U Drain is formed between the outer shutters and the inner core of the mould. The space between these components determines the concrete wall thickness, base thickness and internal channel profile.
The inner core must remain centred, straight and correctly positioned throughout concrete placement and vibration. If it shifts toward one side, one wall may become thicker while the opposite wall becomes thinner.
Accurate inner-core centring helps manufacturers produce consistent U Drains with matching walls, correct internal openings and cleaner demoulding.
What Is a U Drain Mould Inner Core?
The inner core is the iron or steel forming component that creates the internal channel of a precast U Drain.
Depending on the mould design, it may be:
• Fixed • Removable • Folding • Collapsible • Shrinkable • Hinged • Mechanically operated • Hydraulically operated
A folding or shrinkable design creates clearance between the concrete and the forming surface before removal.
Main Components of an Inner-Core System
A heavy-duty iron inner-core assembly may include:
• Steel forming plates • Structural stiffeners • Main supporting frame • Hinged side sections • Folding mechanism • Pivot pins • Bushes • Mechanical locks • Hydraulic cylinders where specified • Locating stops • Alignment blocks • End guides • Core-support brackets • Joint-sealing surfaces
Every component can affect the final position of the core.
Why Core Centring Is Important
Correct inner-core centring helps maintain:
• Equal wall thickness • Correct internal channel width • Consistent base thickness • Straight drain walls • Symmetrical U Drain profile • Proper reinforcement cover • Accurate end-joint profiles • Smooth demoulding • Better site alignment • Repeatable production quality
An off-centre core can affect the structural and dimensional requirements of the drain.
Understanding Wall Thickness
The wall thickness is determined by the distance between the outer shutter and the inner-core forming surface.
The two walls should match the approved U Drain drawing.
Wall thickness can vary when:
• The core is shifted sideways • An outer shutter is misaligned • A core section is bowed • A locating stop is worn • Reinforcement pushes the core • Locks apply uneven force • Concrete pressure moves the core • The mould bed is not level
Measurements should be taken at several positions along the mould.
Understanding Base Thickness
Base thickness is formed by the vertical clearance between the lower inner-core surface and the mould base.
Incorrect core height may cause:
• Excessive base thickness • Insufficient base thickness • Uneven internal channel depth • Incorrect reinforcement cover • Poor connection with adjoining units • Increased material variation
Core height should be checked from fixed mould references.
What Is Core Taper?
Taper is a controlled change in profile that helps the inner core release from the hardened concrete.
Depending on the approved product and mould design, taper may be provided:
• Along internal drain walls • Across the core height • At profile transitions • Near end-joint formers • On removable core sections
The taper should follow the approved product and mould drawing.
Why Taper Matters
Correct taper can help:
• Reduce concrete binding • Lower demoulding force • Protect concrete edges • Support smooth core withdrawal • Reduce mould wear • Prevent surface scratching • Improve production repeatability
Too little release geometry may cause sticking, while an incorrect or excessive taper can change the required drain profile.
Do not modify the taper without design approval.
What Are Inner-Core Clearances?
Clearance is the controlled space provided for:
• Core installation • Folding or shrinking movement • Shutter closing • Joint operation • Demoulding • Hinge movement • Reinforcement placement • End-former engagement
Clearance does not mean uncontrolled looseness. Excessive mechanical play can allow the core to shift during casting.
Common Signs of an Off-Centre Core
Possible signs include:
• Different left and right wall thicknesses • Internal channel shifted sideways • Uneven top-wall widths • Reinforcement cover variation • One side difficult to demould • Repeated concrete edge damage • Uneven joint-former profile • Core rubbing against one shutter • Different joint gaps on opposite sides • Asymmetrical finished drain
Repeated defects should be recorded according to mould position.
Common Causes of Inner-Core Misalignment
The core may become misaligned because of:
• Worn locating pins • Damaged alignment blocks • Loose core supports • Bent forming plates • Worn hinges or bushes • Unequal locking • Cylinder synchronization problems • Slurry buildup • Mould-bed settlement • Incorrect end-guide position • Impact during handling • Reinforcement interference • Previous repair distortion • Concrete pressure during filling • Excessive vibration
The complete mould system should be inspected before adjusting one component.
Preparing the U Drain Mould for Inspection
Before checking the core:
• Empty and clean the mould • Isolate electrical power • Release hydraulic pressure • Secure hydraulic controls • Mechanically support the inner core • Open outer shutters where required • Remove concrete and slurry • Clean locating points • Review the approved drawings • Identify the original mould datums • Prepare suitable measuring tools
Never enter the mould or work below a core supported only by hydraulics.
Establishing a Fixed Datum
Measurements should be taken from verified mould references.
Suitable datums may include:
• Mould-bed centreline • Fixed base-frame edge • Machined reference stop • Verified outer-shutter face • Mould-bed elevation point • End-frame centreline
Do not measure only from a movable shutter that has not been checked.
Marking the Mould Centreline
A visible centreline helps compare the core position with the base frame and outer shutters.
The centreline may be transferred to:
• Mould bed • End frame • Core support • End shutter • Alignment jig
The same fixed reference should be used during future inspections.
How to Check Core Centring
A general centring inspection may include:
1. Clean the Mould
Remove all buildup from forming and locating surfaces.
2. Lock the Core in Casting Position
Use the approved operating sequence.
3. Verify the Base-Frame Centreline
Confirm the reference marks have not moved.
4. Measure Left-Side Spacing
Check the distance between the core and outer shutter at several points.
5. Measure Right-Side Spacing
Take corresponding measurements at the same stations.
6. Compare Both Sides
Identify side shift, taper variation or local bowing.
7. Check Core Height
Measure its position relative to the mould bed.
8. Check End Positions
Confirm the core enters end guides correctly.
9. Inspect Diagonals
Check for twist or skew.
10. Record the Results
Compare measurements with the approved mould drawing.
No generic tolerance should be assumed.
Measurement Locations
Check spacing at:
• Both ends • Middle of the mould • Intermediate support points • Upper wall region • Lower wall region • Base corners • Folding joints • End-former transitions
Checking only at one end can miss a bowed or angled core.
Checking Equal Wall-Thickness Spacing
The cavity width between the inner core and outer shutter should correspond to the approved concrete wall thickness.
Check:
• Left and right sides at matching stations • Upper and lower regions • Areas between stiffeners • Locations near locks • End-shutter transitions • Joint-former areas
Different readings may result from movement of the core, outer shutter or both.
Checking Base Clearance
Core-to-base clearance determines the base thickness.
Inspect:
• Both ends • Centre • Cross-support positions • Areas near hydraulic cylinders • Folding-core transitions • Locations with previous thickness defects
A low core may reduce the cavity below it, while a high core may increase the base thickness.
Checking Core Straightness
A core may be centred at its ends while bowing in the middle.
Straightness may be checked using:
• Laser alignment • Tensioned reference line • Verified straightedge • Surveying equipment • Approved inspection fixture
Inspect both the top reference and side forming surfaces.
Checking Core Twist
Core twist may cause:
• Unequal wall spacing at different heights • Incorrect corner geometry • Binding during folding • Uneven end-guide contact • Difficult demoulding
Twist may be identified using:
• Cross-level readings • Diagonal measurements • Corner elevations • End-frame comparisons • Laser-reference planes
Do not force the outer shutters closed to compensate for a twisted core.
Checking Core Taper
Core taper should be measured against the approved profile.
Possible methods include:
• Approved profile template • Section gauge • Measurement at defined heights • Laser scanning where available • Comparison with mould drawings
Check the taper at both ends and through the middle.
Inspecting Folding or Shrinkable Sections
A folding inner core should move evenly without excessive play.
Inspect:
• Hinges • Pivot pins • Bushes • Folding plates • Linkages • Mechanical stops • Locks • Hydraulic cylinders • Joint gaps • Forming-surface continuity
Excessive hinge wear can change the core profile in its casting position.
Inspecting Locating Pins and Stops
Locating components establish repeatable core position.
Check for:
• Bent pins • Worn bushes • Enlarged holes • Loose stops • Impact marks • Slurry buildup • Cracked mounting welds • Incomplete seating • Unequal contact
A worn locating pin can allow movement during vibration.
Inspecting Core Supports
Core-support brackets transfer the core load to the mould frame.
Check:
• Support height • Bearing contact • Loose fasteners • Cracked welds • Bent brackets • Damaged adjustment points • Uneven shims • Movement marks • Corrosion • Previous repair distortion
Improvised packing should not be used as a permanent support.
Hydraulic Core Alignment
Where the core is hydraulically operated, inspect:
• Cylinder mounting • Stroke consistency • Hose condition • Pivot-pin wear • Synchronization • Mechanical stops • End-position alignment • External leakage • Control-valve operation • Mechanical safety supports
Hydraulic pressure should not be used to hold the core against an incorrect mechanical stop.
Reinforcement Clearance
The reinforcement cage should fit between the core and outer shutters without forcing either component out of position.
Check:
• Cage dimensions • Required concrete cover • Spacer condition • Bar alignment • End-joint clearance • Lifting-insert position where approved • Tie-wire location • Clearance during shutter closing
Do not cut, bend or relocate reinforcement without engineering approval.
How Reinforcement Can Shift the Core
Core movement may occur when:
• Bars are too wide • Spacers are unstable • Cage is not centred • Tie wire becomes trapped • Reinforcement contacts the folding mechanism • Concrete placement moves the cage • Outer shutters force the cage inward
Complete a clearance check before locking the mould.
Joint Former and Core Alignment
Tongue-and-groove or other joint formers should remain centred on the internal channel.
Check:
• Former centreline • Core-to-former transition • Left and right wall relationship • End-shutter position • Profile continuity • Demoulding direction • Slurry-sealing contact
A centred core with a misaligned joint former can still produce an unusable drain end.
Applying Mould Release Agent
Apply release agent after the mould is cleaned and aligned.
The coating should be:
• Thin • Uniform • Present on all forming surfaces • Applied around folding joints • Applied near profile transitions • Free from excessive pooling • Kept away from reinforcement
Release agent should not be used to hide a rough or damaged forming surface.
Pre-Pour Core Inspection Checklist
Before placing concrete, confirm:
• Core is clean • Correct core profile is installed • Folding mechanism operates smoothly • Casting-position locks are engaged • Core centreline matches the mould datum • Left and right spacing is verified • Base clearance is checked • Taper matches the approved drawing • End guides are seated • Outer shutters are aligned • Joint formers are correctly positioned • Reinforcement has adequate clearance • Hydraulic systems are in approved condition • No tools remain inside the mould
Measurements should be recorded where required by the quality plan.
Concrete Placement Around the Core
Concrete should be placed evenly on both sides of the core.
Uneven filling can create temporary pressure that pushes the core sideways.
Good practices include:
• Alternate placement between sides • Maintain similar concrete levels • Avoid dumping the complete load on one side • Prevent direct impact on the core • Monitor locks and supports • Keep reinforcement stable • Observe for core movement • Follow the approved casting sequence
The placement method should suit the mould configuration.
Concrete Vibration and Core Movement
Vibration can loosen an inadequately secured core.
Before vibration:
• Check every core lock • Confirm locating pins • Inspect supports • Verify outer-shutter locks • Confirm hydraulic/mechanical stops • Remove loose tools
During vibration, observe for:
• Core movement • Unequal joint gaps • Lock movement • Slurry leakage • Unusual metallic noise • Outer-shutter displacement
Stop the process safely if significant movement occurs.
Preparing for Demoulding
Before releasing the inner core:
• Confirm adequate concrete strength • Support the U Drain unit • Isolate hydraulic and electrical systems as required • Remove concrete around locks • Identify the approved folding sequence • Mechanically support moving sections • Keep personnel clear of pinch points • Prepare approved handling equipment
Actual demoulding strength and timing should follow the concrete and production procedures.
Correct Inner-Core Release Sequence
The exact procedure depends on the mould design. A general sequence may include:
1. Release Secondary Locks
Remove locks that do not support the main core position.
2. Activate the Designed Shrinking Mechanism
Create clearance progressively.
3. Confirm Both Sides Release
Check that one side has not remained locked.
4. Fold or Retract the Core
Follow the approved movement sequence.
5. Observe Concrete Corners
Ensure the core separates without dragging.
6. Withdraw or Lift the Core Safely
Use approved support and handling points.
7. Protect U Drain Edges
Keep the steel core away from fresh concrete corners.
8. Inspect the Finished Channel
Check wall thickness, finish and symmetry.
Do not force a core that has not fully released.
Why an Inner Core Becomes Stuck
Possible causes include:
• Insufficient taper • Poor release-agent coverage • Concrete fins • Damaged folding mechanism • Core distortion • Incorrect release sequence • Slurry buildup • Worn hinges • Incomplete shrinking • Early concrete cracking • Reinforcement interference • Incorrect concrete strength at demoulding
The cause should be identified before applying additional force.
Post-Demoulding U Drain Inspection
Inspect the finished product for:
• Left wall thickness • Right wall thickness • Base thickness • Internal opening • Channel centreline • Wall straightness • Taper • Joint profile • Concrete cover • Surface finish • Honeycombing • Edge damage • Cracks
Record results according to mould position.
Troubleshooting Common Problems
Problem: One Wall Is Thicker Than the Other
Possible causes:
• Core shifted sideways • Outer shutter is misaligned • Locating stop is worn • Reinforcement pushed the core • Concrete was placed unevenly
Problem: Wall Thickness Changes Along the Drain
Possible causes:
• Core is bowed • Outer shutter is not straight • End guides are misaligned • Support brackets differ in position • Mould bed is distorted
Problem: Base Is Thicker at One End
Possible causes:
• Core height is uneven • Base frame is not level • Core support has settled • Hydraulic cylinders are mismatched • Core is tilted longitudinally
Problem: Core Is Difficult to Fold
Possible causes:
• Slurry buildup • Hinge-pin wear • Damaged bush • Linkage misalignment • Concrete fin • Incorrect lock release • Distorted folding plate
Problem: Concrete Edge Breaks During Core Removal
Possible causes:
• Concrete strength is insufficient • Core was not fully retracted • Release agent is missing • Core taper is damaged • Withdrawal direction is incorrect
Problem: Internal Channel Is Twisted
Possible causes:
• Core is twisted • End frames are misaligned • Base supports have moved • Folding sections are not locked evenly • Previous repair distorted the core
Inner-Core Maintenance Checklist
After every casting cycle:
• Clean all forming surfaces • Remove slurry from folding joints • Inspect hinges and bushes • Check pivot pins • Inspect locks • Clean locating pins and stops • Check support brackets • Inspect hydraulic cylinders where fitted • Check forming-plate straightness • Examine welds and stiffeners • Confirm folding movement • Apply corrosion protection during storage • Record recurring dimensional defects
Do not allow concrete to harden inside moving joints.
Benefits of Accurate Inner-Core Centring
Correct centring provides:
• More equal wall thickness • Consistent base thickness • Symmetrical internal channel • Better reinforcement cover control • Cleaner joint profiles • Easier demoulding • Reduced edge damage • Lower product rejection • Improved drain alignment • Longer mould-component life
Conclusion
The inner core is the main component that forms the internal channel of a precast U Drain. Its centreline, height, taper and mechanical clearances directly affect wall thickness, base thickness and demoulding performance.
A reliable inspection should compare the core with fixed mould datums at both ends, the middle and all critical support locations. Folding mechanisms, locating pins, supports, end guides and outer shutters should also be checked because each can influence core position.
An accurately centred heavy-duty iron U Drain mould helps manufacturers produce symmetrical drainage units with consistent walls, correct internal profiles and reliable production quality.